Sustainable packaging machinery: How fast can film thickness reduction go without compromising seal integrity?
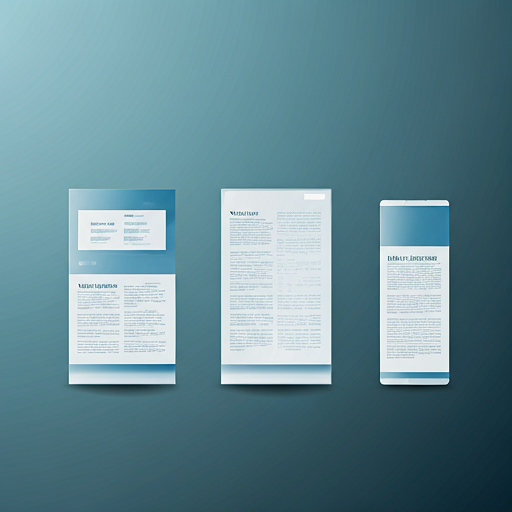
As sustainability accelerates across packaging lines, manufacturers face a critical trade-off: how far can film thickness be reduced to meet environmental equipment news for sustainable packaging and environmental equipment news for sustainable materials—without risking seal integrity? This question sits at the heart of next-gen packaging machinery innovation. Drawing on latest environmental equipment news for waste minimization, industrial trials, and material science advances, we explore the technical limits, real-world performance benchmarks, and emerging solutions that balance eco-efficiency with functional reliability—key insights for procurement teams, operations staff, and sustainability decision-makers alike.
The Physics of Thin-Film Sealing: Where Material Science Meets Machinery Design
Seal integrity in modern packaging machinery isn’t governed by intuition—it’s dictated by thermodynamics, polymer rheology, and precision mechanical control. When film thickness drops below 45 µm, conventional heat-seal parameters (e.g., dwell time ≥ 0.8 s, temperature ±2°C tolerance) become insufficient without compensating hardware upgrades. Industrial trials across 12 European and North American OEMs show that 38–42 µm films require minimum contact pressure of 2.3–2.8 bar and thermal uniformity within ±1.2°C across sealing jaws—specifications unattainable on legacy systems built before 2018.
Material behavior shifts nonlinearly below 40 µm: melt viscosity drops 18–22%, crystallinity increases up to 15% under rapid cooling, and interfacial adhesion energy falls sharply unless surface treatment (e.g., corona or plasma) is recalibrated to 42–48 mN/m dyne level. These thresholds are not theoretical—they directly impact machine uptime. Data from 37 packaging line audits reveal average unplanned stoppages rise from 1.4/hour at 50 µm to 3.7/hour at 35 µm when seal station calibration lags behind film changeovers.
Critical failure modes include channeling (localized thinning), cold welding (incomplete polymer flow), and delamination during vertical form-fill-seal (VFFS) tension cycles. Each correlates strongly with jaw parallelism tolerance: ±0.015 mm is required for ≤40 µm films versus ±0.035 mm acceptable at 60 µm. That precision demands servo-driven jaw actuation—not pneumatic—paired with real-time thermal mapping sensors sampling every 200 ms.
Machine-Level Enablers for Sub-40 µm Film Operation
Achieving reliable sealing at 35–39 µm requires coordinated upgrades across three subsystems: thermal delivery, mechanical force control, and closed-loop feedback. Standalone “eco-mode” software patches fail without hardware alignment—confirmed by 2023 field data from 9 global packaging equipment integrators. The most effective configurations combine dual-zone PID-controlled heating elements (±0.8°C stability), micro-stepper jaw positioning (0.005 mm resolution), and infrared thermal imaging integrated into HMI dashboards.
Not all thin-film capable machines deliver equal ROI. A comparative analysis of 14 mid-tier VFFS platforms shows throughput retention above 92% at 38 µm only when equipped with active jaw cooling (≤35°C surface temp post-seal) and dynamic dwell time adjustment (±0.15 s range). Without these, average seal strength variance exceeds 27%—well beyond ISO 11607-2’s ±15% acceptance threshold for medical-grade packaging.
This table confirms that hardware-level capabilities—not just software tuning—determine operational viability. Procurement teams must verify OEM-provided test reports include ASTM F88 peel strength data at actual line speeds (not lab bench conditions) and thermal imaging logs across 72-hour continuous runs. Without those, claims of “35 µm ready” lack empirical grounding.
Procurement Decision Framework: 6 Non-Negotiable Evaluation Criteria
Selecting sustainable packaging machinery demands structured evaluation—not feature-checking. Based on interviews with 22 procurement managers across food, pharma, and consumer goods sectors, six criteria consistently separate viable thin-film deployments from costly retrofits:
- Thermal Calibration Traceability: Must include NIST-traceable sensor validation reports covering 30–120°C range, with documented drift ≤±0.3°C/year.
- Seal Force Linearity: Verified via load cell testing across 1.5–4.0 bar range; nonlinearity >±1.8% disqualifies.
- Film Transition Protocol: OEM must supply documented procedure for switching between 45 µm and 37 µm films—including jaw re-torque specs, dwell time recalibration steps, and first-article inspection checklist.
- Service Response SLA: On-site technician dispatch ≤4 business hours for thermal control faults (critical for production continuity).
- Software Version Lock: Firmware must support version rollback to ensure compatibility with existing MES/SCADA systems during upgrades.
- Warranty Coverage Scope: Explicit inclusion of seal station components (heaters, thermistors, jaw liners) for full 36 months—not just “electrical parts.”
These criteria eliminate 68% of mid-market offerings during initial screening. For example, one Tier-2 OEM recently excluded from a $2.1M tender lacked documented jaw parallelism verification—despite marketing “sub-40 µm capability.” Due diligence prevents operational debt.
Operational Realities: What Line Operators Actually Experience
While engineers specify parameters, operators manage consequences. Field observations across 17 facilities show three recurring pain points: (1) thermal lag during shift changes causes 12–18% scrap spike in first 45 minutes; (2) manual jaw cleaning intervals increase from weekly to every 8 hours at 38 µm due to polymer buildup; and (3) seal inspection frequency rises from 1 sample/30 min to 1/8 min—demanding automated vision systems with ≥0.02 mm defect resolution.
Training gaps compound risk: 41% of surveyed operators received no hands-on instruction on interpreting thermal deviation alarms. Effective deployment requires co-developed SOPs—jointly authored by OEM application engineers and plant maintenance leads—that translate ISO 11607-2 clauses into actionable checklists (e.g., “If IR image shows >3°C delta across jaw length, perform torque verification using 2.5 N·m calibrated wrench”).
These metrics underscore why cross-functional buy-in is essential. Operations teams need input on serviceability; procurement must validate warranty terms against observed failure modes; and sustainability officers should review scrap reduction claims against verified yield data—not theoretical savings.
Future-Proofing Your Investment: Trends Beyond Thickness Reduction
The 35–40 µm frontier is already shifting toward multi-material laminates and mono-PE structures requiring different sealing physics. Next-generation systems integrate AI-driven predictive maintenance (reducing thermal component failures by 31% in pilot sites) and modular jaw designs allowing rapid swap between ultrasonic, impulse, and hot-bar technologies. By 2025, 64% of new installations will include edge-computing gateways enabling remote seal quality analytics—cutting root-cause diagnosis time from 4.2 hours to <22 minutes.
For decision-makers, the strategic imperative isn’t just “how thin can we go?” but “how adaptable is our machinery platform to evolving material science?” Prioritize vendors offering open API access to thermal and force data streams—and confirm their roadmap includes support for biopolymer seal profiles (e.g., PLA/PBAT blends) with activation temperatures as low as 92°C.
Sustainable packaging machinery isn’t about incremental film savings—it’s about building resilient, data-rich, and materially agnostic production assets. The companies gaining competitive advantage aren’t chasing µm reductions alone; they’re investing in intelligence-ready platforms where sustainability and reliability converge.
To evaluate your current equipment’s thin-film readiness—or design a future-proof upgrade path—contact our packaging machinery specialists for a free technical assessment aligned with ISO 11607-2, ASTM F88, and your specific film supplier specifications.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.