Production Planning for Factories: How to Cut Delays and Improve Output
Why production planning for factories now starts with operational context
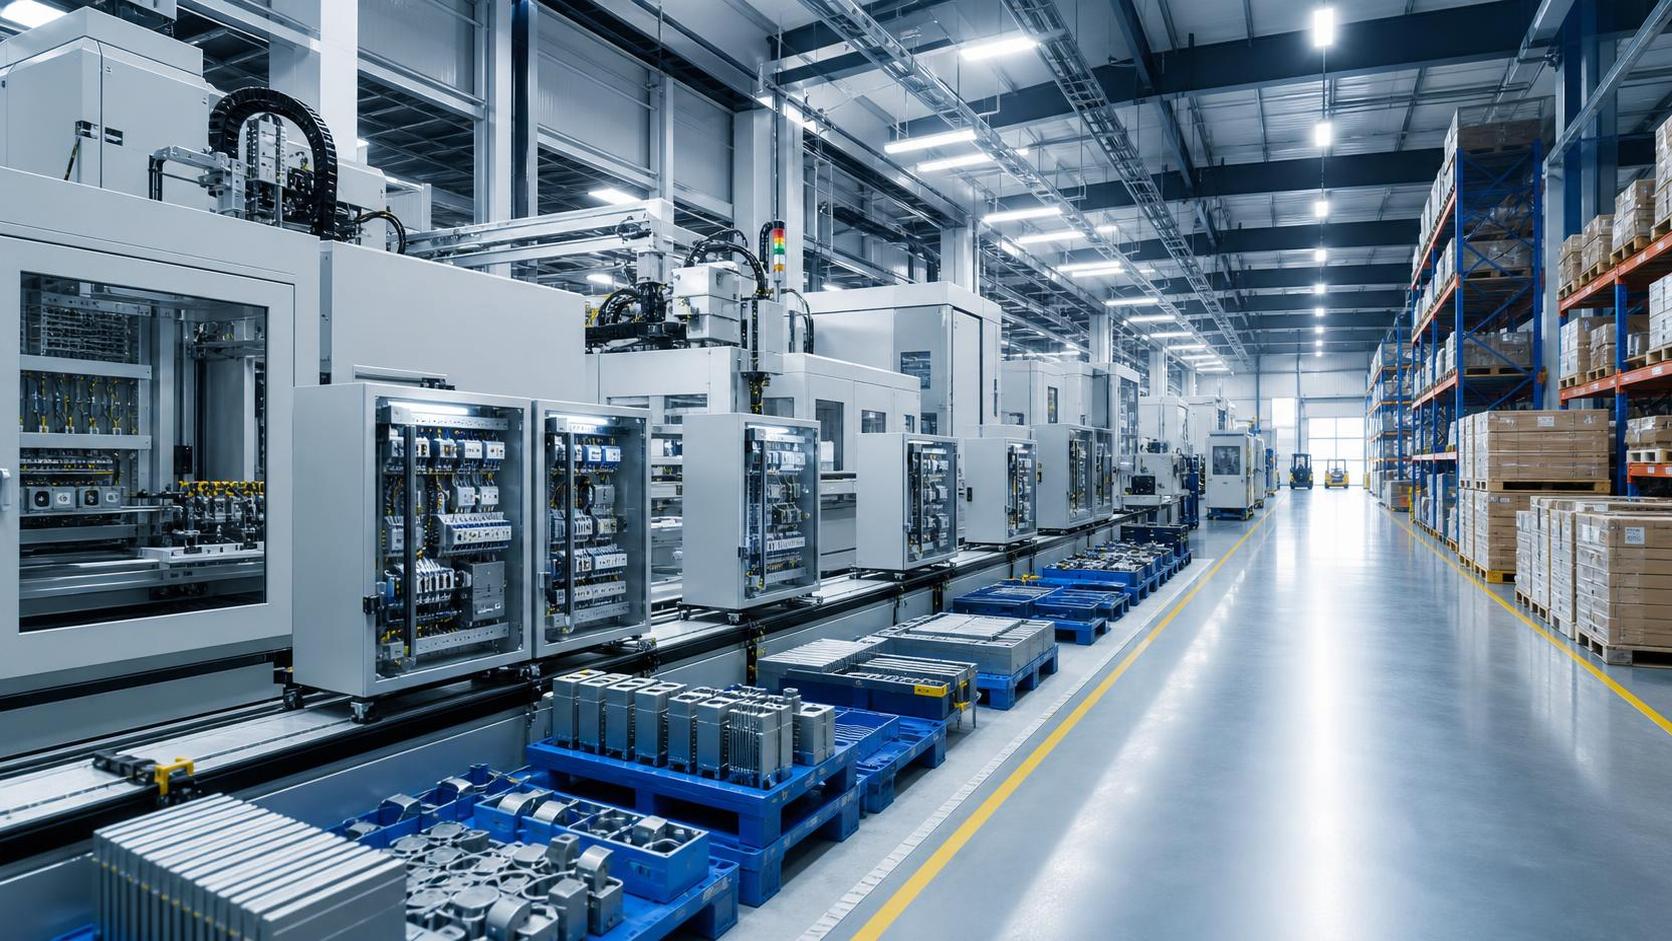
Production planning for factories now shapes delivery reliability, working capital, and plant responsiveness, not just daily machine loading.
When orders shift quickly, raw material lead times stretch, or equipment uptime becomes unstable, weak planning shows up as delay, expediting, and avoidable output loss.
In actual operations, the same planning method rarely fits every plant. A mixed-model assembly line needs different control logic than a batch machining workshop.
That is why production planning for factories should be judged by scenario fit. Demand volatility, component risk, routing complexity, and changeover time all matter.
Across industrial machinery, electrical equipment, automation systems, and mechanical components, the planning challenge is similar, but the bottlenecks are not.
A practical planning structure helps cut delays, stabilize release decisions, and improve output without forcing excess inventory into the system.
Different factory settings create different planning priorities
Production planning for factories often fails when similar-looking operations are treated as identical. The routing may look close, but constraints can be completely different.
A plant producing standard electrical cabinets usually plans around repeatability, supplier coordination, and takt consistency. A custom equipment builder plans around engineering release dates.
In export-driven sectors, planning also depends on shipment windows, compliance timing, and packaging readiness. Missing one external milestone can erase internal efficiency gains.
More often, the decisive question is not whether capacity exists on paper. It is whether capacity is usable at the right time, with the right material, tooling, and labor mix.
Industrial market intelligence also changes planning assumptions. Policy shifts, exhibition-driven demand spikes, and supplier concentration can alter what a realistic plan looks like.
Where planning pressure usually comes from
- Order mix changes faster than scheduling rules can absorb.
- Critical parts arrive late, even when common materials are available.
- Changeovers consume more time than standard capacity models assume.
- Engineering revisions release in stages, disrupting planned sequences.
- External logistics deadlines override internal production preferences.
High-volume repeat production needs flow discipline, not just bigger schedules
For repeat production, production planning for factories should focus on line balance, replenishment timing, and small disruptions that accumulate into missed output.
This is common in power supplies, standard enclosures, connectors, and other products with stable demand but tight delivery expectations.
The planning mistake here is overvaluing aggregate monthly capacity. Output loss usually begins with hourly imbalance, feeder shortages, or unplanned micro-stoppages.
A better approach is shorter planning cycles with clear frozen windows. That keeps sequencing stable while leaving controlled flexibility for urgent orders.
It also helps to separate true bottleneck assets from supportive resources. If the bottleneck is clear, buffer placement becomes more rational.
What to judge in this setting
Look at actual changeover loss, recovery speed after stoppages, and shortage frequency by component family. These indicators usually explain delay better than utilization alone.
Production planning for factories in repeat environments should also align with supplier call-off reliability. Stable output depends on stable inbound rhythm.
Custom equipment and engineered orders require milestone-driven planning
In engineered-to-order production, delays often start before manufacturing. Drawings, bill of materials maturity, and approval gates shape the real production calendar.
This is typical in automation systems, industrial skids, process equipment, and EPC-linked fabrication where every order carries configuration differences.
Here, production planning for factories should be built around release confidence, not optimistic demand dates. Premature scheduling creates false commitments and repeated rescheduling.
A useful practice is to split planning into engineering release milestones, long-lead procurement control, fabrication loading, and final integration windows.
That structure makes hidden dependencies visible. It also prevents assembly areas from becoming storage zones for incomplete jobs.
A common misread in project-based factories
Many teams assume that similar projects can share the same standard lead time. In practice, one late electrical component or software interface can shift the entire sequence.
Production planning for factories in this setting needs risk tags by job, not just due dates by order.
When supply chain uncertainty dominates, planning must protect critical paths
Some factories have enough internal capacity, but still miss output because imported parts, castings, semiconductors, or specialty drives arrive unpredictably.
In these situations, production planning for factories should shift from broad schedule optimization to critical-path protection and scenario-based allocation.
That means identifying which shortages stop shipment, which only reduce efficiency, and which can be engineered around with approved alternatives.
Industrial information platforms often help here by tracking supplier developments, trade policy changes, exhibition activity, and regional market shifts that affect availability.
Planning becomes stronger when external signals are reviewed alongside internal inventory status. A material shortage rarely appears without warning.
Multi-site and export programs need planning tied to shipment reality
Production planning for factories becomes more complex when output must move across plants, ports, integrators, or regional warehousing channels.
A factory may finish production on time and still fail the customer timeline because documentation, inspection, packaging, or vessel cutoff was missed.
This is especially relevant in industrial export activity, where compliance checks and international logistics often compress the available dispatch window.
The planning response should include backward scheduling from shipment milestones, not only forward loading from workshop capacity.
Where multiple factories feed one project, version control and transfer timing matter as much as machine utilization.
Practical checks before release
- Confirm whether packaging materials and inspection slots are constrained resources.
- Check if outbound dates are fixed or negotiable before prioritizing rush jobs.
- Review whether inter-plant transfers depend on external carriers or customs documents.
- Separate commercial delivery promise dates from physically shippable dates.
Where production planning for factories is often misjudged
One common error is treating planning software output as operational truth. A digital schedule is useful, but only if routing, labor assumptions, and shortages are current.
Another mistake is focusing only on procurement price. A lower-cost part with unstable lead time can create larger losses than a higher-cost stable source.
Production planning for factories also suffers when maintenance calendars stay outside planning logic. Uptime assumptions then become too optimistic.
Similar-looking orders can mislead planners as well. A mechanical assembly and an electrically tested unit may share structure, yet require very different release timing.
In real facilities, bottlenecks move. A welding cell may constrain one month, then final test benches become the real limiter after order mix changes.
How to build a more reliable planning routine from here
A stronger routine starts with segmenting the factory by planning behavior, not by department chart alone. Repeat flow, project work, and shortage-driven orders need separate rules.
Then define a small set of control points: material readiness, release maturity, bottleneck loading, quality hold risk, and shipment readiness.
Production planning for factories improves when these control points are reviewed at fixed intervals and tied to clear escalation actions.
It also helps to compare internal performance with external market movement. Equipment trends, supplier changes, and trade signals often explain why old assumptions stop working.
That is where broader industrial intelligence becomes useful. It supports planning decisions with context, especially when sourcing risk or regional demand begins to shift.
The next step is practical: map current production scenarios, identify which delays repeat, and link each delay to a planning condition rather than a general efficiency target.
From there, compare lead times, capacity assumptions, and supply constraints by scenario. That creates a more dependable basis for improving output and reducing delays.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.