How to Select Mechanical Components for Load, Speed, and Service Life
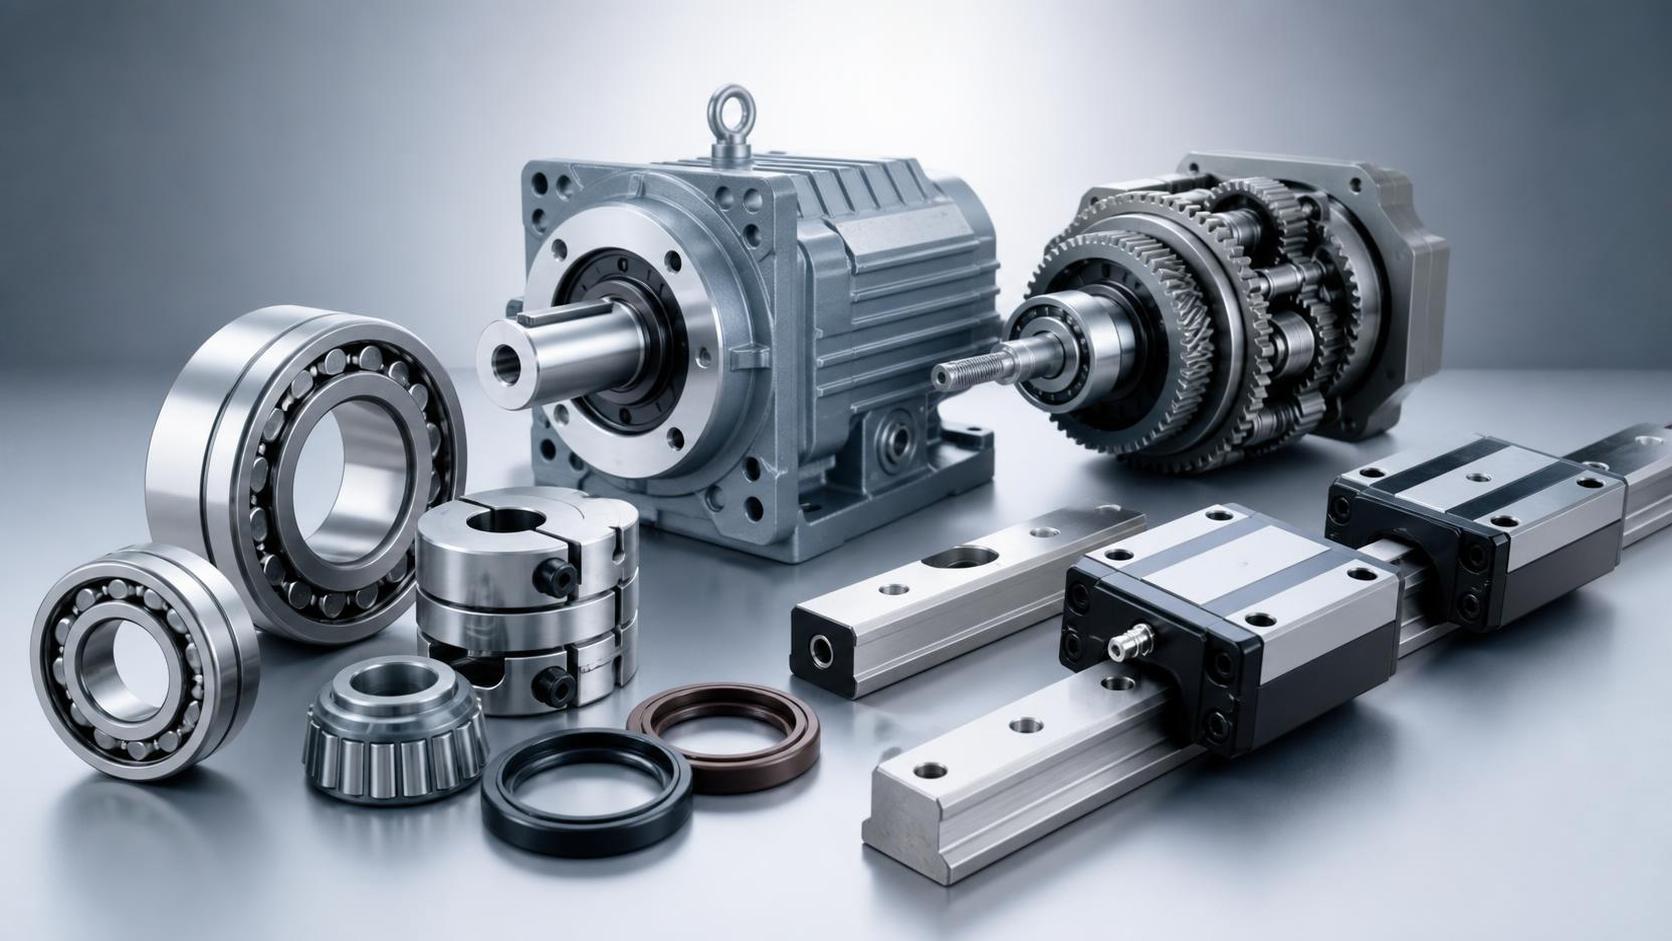
Selecting mechanical components sounds straightforward until a machine has to carry real load, run at real speed, and survive for years under variable operating conditions. That is where many evaluations break down. Teams often compare catalog values, confirm dimensional fit, and move on, only to discover later that the chosen bearing, coupling, gearbox, seal, guide, or transmission element performs well in one dimension while failing in another. For technical evaluators, the real task is not to identify a component that can work in theory, but to identify one that can continue working in the actual duty profile of the equipment, with acceptable maintenance, risk, and lifecycle cost.
The search behind this topic is usually practical: how to judge tradeoffs before a bad decision gets locked into production, procurement, or installation. Load, speed, and service life are the core variables, but they are not independent. Pushing one typically constrains the others. A component that handles high static load may run poorly at sustained high speed. A design optimized for compactness may lose service life under shock loading. A low-cost option may meet nominal ratings yet require replacement intervals that erase any purchase-price advantage.
Start with the duty profile, not the catalog headline
The most common selection mistake is treating a maximum rating as an operating recommendation. In practice, technical evaluation should begin with the duty profile of the machine or subsystem:
- What load is continuous, and what load is occasional?
- Is the load radial, axial, torsional, bending, or combined?
- Is the speed constant, variable, indexed, or subject to frequent starts and stops?
- What is the expected operating schedule: single shift, multi-shift, or near-continuous service?
- How much shock, vibration, misalignment, contamination, or thermal cycling is present?
These questions matter because many mechanical components fail from real operating patterns rather than headline overload. A linear guide in a clean lab environment and the same guide on a dusty packaging line face very different service-life outcomes, even if nominal load looks similar. Likewise, a coupling selected for average torque may still fail if recurring peak torque during startup or reversal is not accounted for.
For technical teams, it is often more useful to document the load spectrum and duty cycle than to debate brand preference too early. If the operating profile is weakly defined, even a premium component can become the wrong choice.
Load assessment: the number that matters is rarely a single number
In industrial selection work, “load” is often reduced to one figure in the specification sheet. That is usually insufficient. A credible assessment separates static load, dynamic load, peak load, and moment load where relevant. It also asks whether the load is steady or fluctuating.
For example, bearings, screws, chains, belts, couplings, and gear drives all respond differently to repeated peak events. A component that survives a short overload in one application may experience accelerated fatigue in another. This is why service factors are widely used, although the exact factor depends on component type, drive characteristics, and operating severity. Using a generic safety margin without understanding the source of loading can create false confidence.
Technical evaluators should also be cautious with load values generated from ideal design assumptions. Actual field conditions often introduce:
- Unexpected side loads from assembly tolerances
- Misalignment caused by base-frame deflection
- Load concentration from uneven contact
- Impact loads from operator behavior or process variation
- Transient spikes from jams, emergency stops, or motor control changes
These are not edge cases. In many industrial systems, they are normal. If the application includes shock or reversing duty, that should be treated as a first-order selection variable, not a footnote.
Speed changes the failure mode, not just the performance envelope
Higher speed is often associated with higher productivity, but from a mechanical standpoint it changes lubrication behavior, thermal buildup, vibration response, and wear mechanisms. This is why components that appear oversized from a load perspective may still underperform at speed.
Take rolling elements and rotating assemblies as an example. At elevated speed, lubrication regime becomes critical. Frictional heat, grease breakdown, cage instability, and sealing limitations can become more important than pure load rating. In power transmission, belts and couplings may encounter dynamic effects, resonance, or tracking issues that do not show up in static calculations. In sliding components, wear rates can accelerate sharply when speed and contact pressure combine beyond the material system’s stable operating range.
The practical implication is that speed should not be treated as a simple “rpm compatibility” check. Evaluators should verify:
- Recommended operating speed versus theoretical maximum
- Lubrication method and relubrication interval
- Heat generation and dissipation path
- Balance quality and vibration sensitivity
- Seal suitability at target speed
- Noise limits if the equipment is operator-facing
Suppliers sometimes present maximum speed values under favorable conditions. Those values are useful, but they are not always representative of continuous industrial duty. If the machine is expected to run near the upper range for long periods, request application-specific confirmation rather than relying on broad catalog interpretation.
Service life is a business variable as much as an engineering one
Service life is often discussed as though it were purely technical, but in B2B decision-making it is inseparable from maintenance strategy, downtime cost, labor availability, and spare-part logistics. A component with shorter theoretical life may still be acceptable in a non-critical, accessible position with low replacement cost. The same component may be a poor choice in an automated line where every maintenance event disrupts throughput and requires specialist labor.
This is where technical evaluators need to move beyond “can it last?” and ask “what happens when it does not?” That means looking at service life in operational context:
- Is failure gradual and detectable, or sudden and disruptive?
- Can the part be replaced during planned maintenance windows?
- Is the component standardized and easy to source globally?
- Does wear affect only the component itself, or does it damage adjacent parts?
- Are lubrication and inspection routines realistic for the end user?
In many sectors, expected life is also shaped by contamination control. Dust, washdown chemicals, metal fines, poor lubrication discipline, and thermal variation shorten life more reliably than many design teams expect. As a result, service-life calculations based on clean, stable conditions should be treated as directional unless field conditions closely match those assumptions.
Do not evaluate components in isolation
Mechanical components rarely fail because one part was inherently defective. More often, they fail because the surrounding system imposed conditions the original selection did not fully address. A gearbox is affected by motor control behavior. A bearing is affected by shaft finish, housing fit, and alignment. A seal depends on surface speed, runout, pressure, and media compatibility. A linear motion assembly depends on mounting rigidity and parallelism.
This system view matters during sourcing as well. Two suppliers may offer similar ratings, but one may provide better tolerance control, lubrication guidance, installation support, and documentation. For a technical evaluator, those factors often have more decision value than minor differences in nominal specification.
It is also worth checking how the chosen component interacts with upstream and downstream constraints. A high-capacity part that requires tighter installation tolerances, special lubrication tools, or long lead times may create hidden cost elsewhere in the project.
Where common selection logic becomes unreliable
Several common assumptions show up repeatedly in industrial procurement and design reviews, and they deserve scrutiny.
“Higher rated means safer”
Not always. Oversized components can introduce inertia, lower efficiency, poor low-load behavior, fitment issues, or unnecessary cost. In some motion systems, excessive sizing can reduce responsiveness or shift stress into adjacent parts.
“If dimensions match, alternatives are interchangeable”
This is risky. Even when envelope dimensions are similar, material grade, heat treatment, surface finish, internal geometry, lubrication design, sealing arrangement, and quality consistency may differ materially.
“Premium brands always justify the extra cost”
Not automatically. In critical, high-duty, hard-to-access, or high-speed applications, the premium may be rational. In less demanding positions, a qualified mid-tier option may deliver better total value. The issue is not brand hierarchy by itself, but application fit and process control.
“Rated life equals real life”
Only under defined assumptions. Actual service life can be much shorter if contamination, misalignment, mounting error, or lubrication discipline is poor. It can also be longer in conservative, clean, stable operations.
A practical evaluation framework for technical teams
For selection decisions that need to hold up across engineering and procurement, a short comparative framework usually works better than a long unstructured specification review. The aim is to make tradeoffs visible early.
Using a framework like this helps prevent selection from being driven by a single variable. It also creates a clearer basis for supplier discussion, especially when comparing options that look similar on paper.
Procurement signals that should influence technical judgment
For many organizations, component selection now sits at the intersection of engineering performance and supply-chain resilience. Technical teams increasingly need to consider whether a part can be sourced consistently across regions, whether documentation is complete, and whether substitute options can be qualified without redesign.
This matters particularly in a broad industrial market where product availability, regional compliance expectations, and logistics costs can shift quickly. Exact regulatory requirements depend on product category and destination market, so any claims around standards, certifications, or trade restrictions should be verified case by case【待核实】. Still, from a decision perspective, the direction is clear: the best component on paper may not be the best component for a production program if it introduces single-source dependence or long replenishment cycles.
Technical evaluators should therefore ask suppliers for more than a datasheet. Useful requests include application references, tolerance documentation, material or heat-treatment consistency information where relevant, recommended installation practices, and clarity on revision control. When the part is business-critical, sample validation under actual duty is usually more informative than extended debate over catalog language.
When field validation is worth the extra time
Not every component choice needs extensive testing, but some conditions justify it. If the application combines high load and high speed, if downtime cost is severe, if the operating environment is dirty or unstable, or if the team is considering a new supplier or substitute design, a controlled validation run can save significant downstream cost.
Field validation does not need to be elaborate. It can focus on measurable indicators such as operating temperature, vibration trend, lubrication condition, wear pattern, torque stability, noise, or replacement interval under real duty. The main objective is to confirm that the selected component behaves as expected in the full system.
That step is especially important when internal stakeholders are under pressure to reduce cost. A lower unit price can be valid, but only if the component preserves reliability where the business actually feels failure: unplanned stoppage, warranty exposure, rushed spare-part orders, and maintenance labor.
The better question is not “Which component is best?”
In most industrial decisions, there is no universally best mechanical component. There is only a more suitable component for a defined load, speed, life target, operating environment, and supply condition. Technical evaluators add the most value when they make those conditions explicit and force the comparison to happen on real duty rather than simplified assumptions.
That usually changes the discussion. Instead of asking whether a part meets the spec, the team starts asking whether the spec reflects reality, whether maintenance can support the design, whether sourcing risk is acceptable, and where the real cost of failure sits. Those are the questions that lead to more durable decisions, especially when machines are expected to run hard, stay available, and remain supportable long after the initial purchase order is closed.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.