How to Evaluate a Switchgear Panel Manufacturer for Utility and Industrial Projects
How to Evaluate a Switchgear Panel Manufacturer for Utility and Industrial Projects
Selecting a switchgear panel manufacturer is not simply a purchasing decision. It determines whether a power distribution project achieves safe commissioning, stable operation, predictable maintenance, and acceptable lifecycle cost.
For project leaders, the right manufacturer is one that can translate operating requirements into a documented, compliant, testable, and supportable electrical solution without creating hidden delivery or integration risks.
The core search intent behind evaluating a switchgear panel manufacturer is practical: buyers need a reliable method to compare suppliers before committing capital, project schedules, and operational continuity.
Utilities, EPC contractors, industrial owners, and project managers usually need more than a catalog comparison. They need confidence that the selected supplier can deliver under real technical, commercial, and site conditions.
Initial price matters, but it is rarely the most important measure. A lower quotation can become expensive when panels fail tests, require redesign, miss delivery milestones, or lack replacement support.
Start with Project Fit, Not the Supplier’s Product Brochure
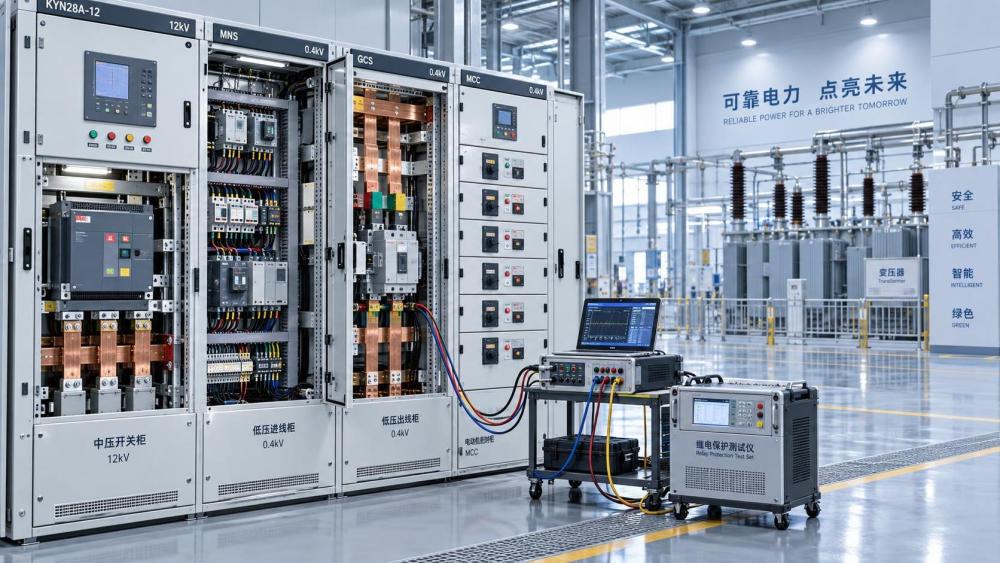
Before reviewing manufacturers, define what the project actually requires. A capable supplier for a small commercial distribution board may not suit a utility substation or continuous-process industrial facility.
Project teams should establish the voltage class, fault level, load profile, environmental conditions, control philosophy, protection requirements, and expected operating life before issuing technical inquiries.
For utility projects, evaluate requirements such as network reliability, remote operation, protection coordination, outage planning, cybersecurity, and future feeder expansion. These requirements often exceed standard industrial panel specifications.
For industrial projects, consider production continuity, motor starting duty, harmonic conditions, hazardous-area interfaces, backup generation, process interlocks, and the consequences of an unplanned electrical shutdown.
A manufacturer should demonstrate that it understands the difference between supplying equipment and engineering a system. This distinction is especially important when switchgear must interface with transformers, relays, SCADA, drives, generators, or existing assets.
Ask suppliers to identify assumptions in their proposal. Clear assumptions reveal engineering discipline, while vague quotations often transfer unresolved technical risk to the buyer later.
The best evaluation process compares manufacturers against a project-specific compliance matrix. This provides a more defensible decision than comparing total price, generic datasheets, or sales presentations.
Verify Engineering Capability and Design Ownership
Engineering capability is one of the strongest indicators of whether a switchgear panel manufacturer can deliver a dependable solution. Review the team responsible for electrical design, mechanical layout, protection, and controls.
Determine whether the manufacturer develops panel designs internally or mainly assembles components according to external drawings. Internal engineering ownership usually improves response time, coordination, and accountability during project changes.
Request examples of similar completed projects with comparable voltage levels, short-circuit ratings, enclosure types, industry applications, and control requirements. Relevant experience is more valuable than a large number of unrelated references.
Evaluate how the supplier handles protection studies, selectivity, relay settings, arc-flash mitigation, and communication architecture. These topics affect both equipment performance and the wider electrical system.
A qualified manufacturer should be able to explain conductor sizing, busbar arrangements, thermal management, dielectric clearances, insulation coordination, and component derating under expected ambient conditions.
For critical applications, ask whether the engineering team uses standardized design libraries, controlled drawings, electrical calculation tools, and formal review gates. Repeatable methods reduce the chance of undocumented design variation.
Project leaders should also assess change-management procedures. Utility and industrial projects frequently evolve, and poorly controlled revisions can cause mismatched wiring, incorrect protection logic, or delayed factory testing.
Ask who approves design changes, how revisions are communicated, and whether updated drawings are issued before fabrication. A disciplined manufacturer maintains a traceable record from approved design through final as-built documentation.
Assess Standards, Certification, and Independent Test Evidence
Compliance claims should always be verified with evidence. The manufacturer must show how its switchgear panels meet applicable IEC, IEEE, ANSI, UL, local grid, customer, and safety requirements.
The applicable standard depends on project geography, voltage level, equipment classification, and client specifications. Do not assume that one certificate covers every panel configuration proposed for the project.
For low-voltage assemblies, request evidence related to IEC 61439 where applicable. For medium-voltage switchgear, review the relevant IEC 62271 or regional standards required by the owner or authority.
Type-test documentation deserves careful attention. Confirm that tested configurations are genuinely representative of the proposed panel, including busbar system, enclosure arrangement, short-circuit capability, internal separation, and temperature-rise performance.
A report from a recognized laboratory is valuable, but it does not eliminate the need for project-specific verification. Component substitutions or altered dimensions can invalidate assumptions based on previous testing.
Ask the manufacturer to identify which requirements are validated through type testing, routine testing, calculation, inspection, or third-party certification. This distinction helps avoid misleading statements about full compliance.
Review certificates for validity, issuing organization, scope, and product model. Expired, incomplete, or unrelated certificates should be treated as warning signs rather than proof of competence.
Where local regulations require approvals, confirm that the supplier understands the approval pathway. Delays in utility acceptance, electrical inspection, or import clearance can affect commissioning even when equipment is technically sound.
Examine Manufacturing Quality Controls Before Award
Good engineering can still fail in production. The manufacturing system determines whether approved drawings become consistent, reliable switchgear panels that can withstand transportation, installation, and years of operation.
Request an overview of the quality management system, including incoming inspection, material traceability, assembly controls, torque verification, wiring checks, calibration records, and nonconformance handling.
ISO 9001 certification can be useful, but project teams should look beyond the certificate. Ask how quality procedures are applied on the shop floor and how deviations are corrected.
Inspect the manufacturer’s control over critical components such as circuit breakers, contactors, relays, busbars, insulation materials, terminals, meters, and communication devices. Unauthorized substitution can create major operational problems.
For utility and industrial applications, verify approved component brands and equivalent-substitution rules. A manufacturer should obtain customer approval before replacing specified components because interfaces, settings, dimensions, and certifications may change.
Factory audits are particularly valuable for high-value or repeat procurement programs. An audit can reveal workshop capacity, cleanliness, segregation practices, test facilities, documentation discipline, and the practical skill level of technicians.
During an audit, observe whether materials are clearly identified, panels are protected from damage, drawings are controlled, and finished equipment is stored appropriately. These details often predict future delivery quality.
Ask how the supplier manages defects discovered after factory testing. Strong manufacturers conduct root-cause analysis and implement corrective actions rather than merely repairing the immediate issue.
Make Factory Acceptance Testing a Commercial Requirement
Factory acceptance testing, or FAT, is the buyer’s most important opportunity to identify defects before equipment reaches the site. It should be defined early, not treated as an optional final event.
The FAT procedure should specify required inspections, tests, witness points, acceptance criteria, documentation, and responsibilities. It should also define how failed items are corrected and retested.
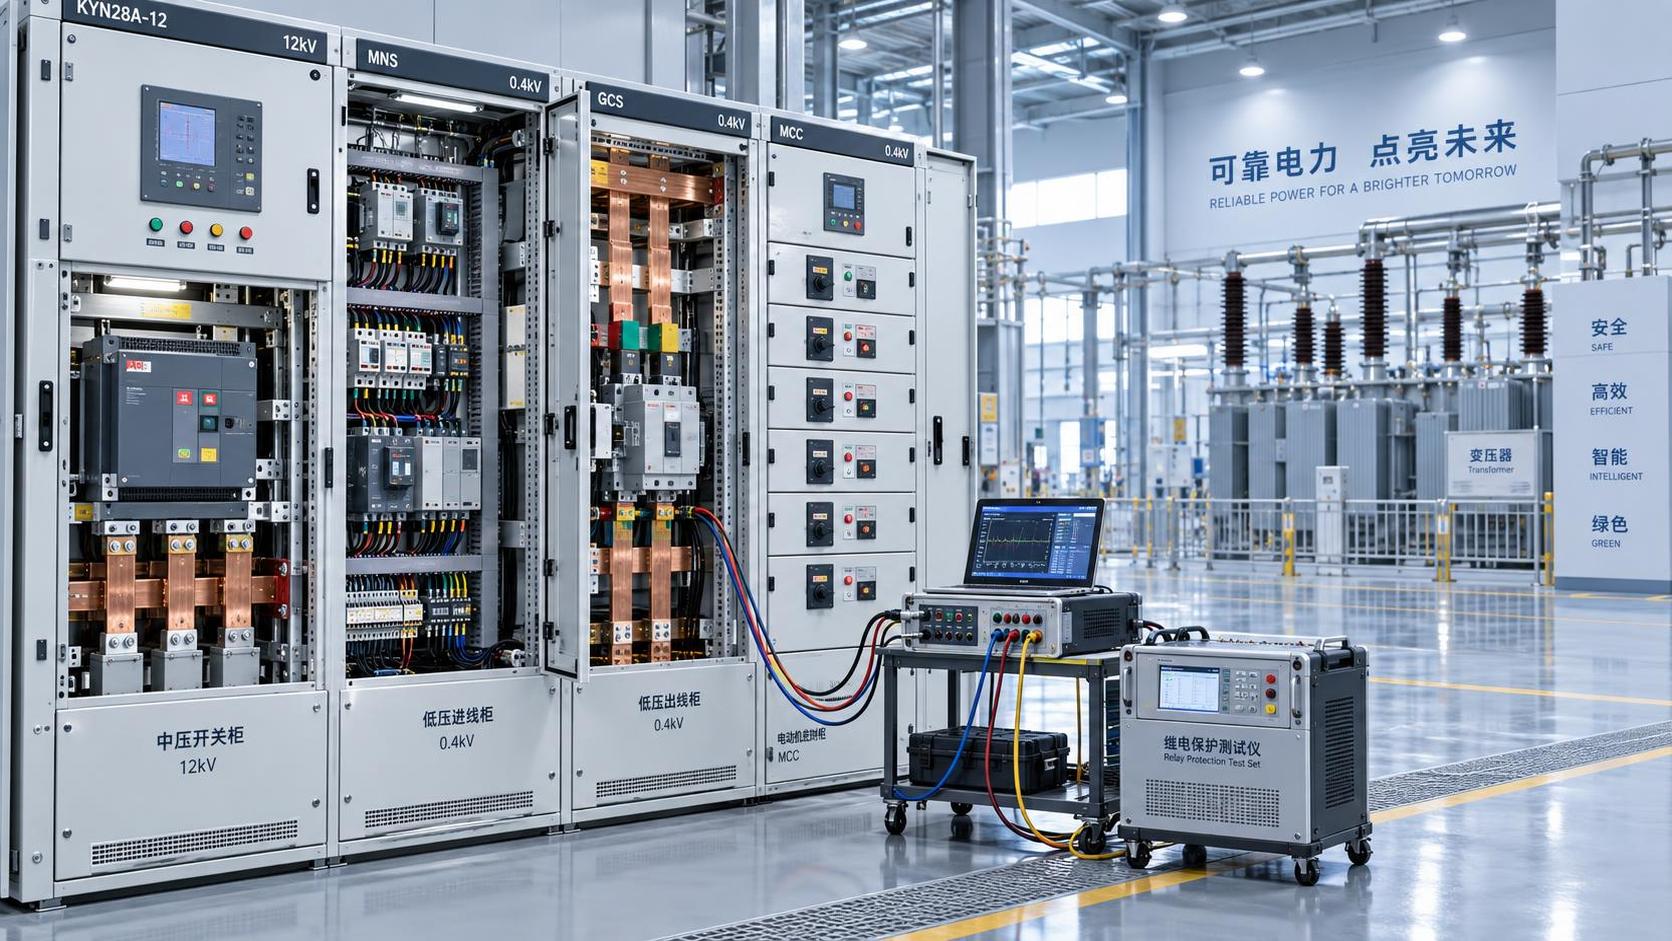
Typical checks include visual inspection, wiring continuity, insulation resistance, dielectric tests, mechanical operation, interlocking verification, protection relay testing, meter validation, and functional control sequence testing.
For automated systems, test communications, alarm signals, remote commands, permissive logic, and failure states. A switchgear panel may pass electrical tests while still failing to perform correctly within the control system.
Project managers should require approved drawings and finalized settings before FAT. Testing against incomplete documents creates ambiguity and can conceal unresolved engineering issues.
Review the manufacturer’s test equipment calibration records and test technician qualifications. Reliable results depend on both competent personnel and instruments that are suitable for the required measurements.
Where practical, attend FAT in person or through a structured remote witness process. Remote participation should include live visual access, test records, panel identification, and a clear mechanism for recording punch-list items.
A credible switchgear panel manufacturer will welcome disciplined FAT requirements because they protect both parties from costly disputes, emergency site work, and last-minute commissioning failures.
Evaluate Delivery Capacity, Supply Chain Resilience, and Schedule Control
Delivery performance is often a decisive factor for utility and industrial projects. Equipment delays can hold up civil works, cable installation, energization, production startup, and contract milestones.
Ask for a realistic manufacturing schedule that separates engineering, approval, material procurement, fabrication, testing, packing, and shipment. A single promised delivery date provides insufficient visibility.
Critical components may have longer lead times than the panel enclosure itself. Circuit breakers, protection relays, current transformers, PLC hardware, and communication modules should be identified early.
Evaluate whether the manufacturer has authorized supply channels, inventory policies, and alternatives for long-lead components. However, alternatives must remain technically approved rather than becoming uncontrolled substitutions.
Request examples of recent on-time delivery performance for comparable projects. Suppliers should be able to explain their schedule tracking method, escalation process, and response when a component delay threatens completion.
For international sourcing, include shipping terms, export packaging, customs documentation, transport insurance, destination requirements, and site delivery constraints in the evaluation. Logistics failures can damage otherwise acceptable equipment.
Consider the supplier’s financial stability and workload. A manufacturer with an overloaded production line, weak cash flow, or heavy reliance on one component source may represent a significant program risk.
Milestone-based reporting is useful after award. It allows project teams to monitor design approval, material availability, fabrication progress, FAT readiness, and shipment rather than discovering delays near the required delivery date.
Compare Total Lifecycle Value Instead of Initial Purchase Price
A lower purchase price does not necessarily produce the lowest project cost. Project leaders should compare total lifecycle value, including installation effort, energy losses, maintenance needs, spares, downtime exposure, and expected service life.
Evaluate enclosure durability, corrosion protection, ingress protection, ventilation design, labeling quality, cable access, and maintainability. These details influence installation time and long-term reliability in real operating environments.
For high-duty applications, ask about rated operating cycles, breaker maintenance intervals, thermal margins, spare capacity, and expandability. Designing only for today’s connected load can create expensive limitations later.
Energy efficiency may also matter, especially for large low-voltage systems with substantial busbar lengths and continuous load. Thermal performance, conductor sizing, and joint quality affect losses and operating cost.
Estimate the consequence of failure for each critical panel. In a process plant, one feeder outage may halt production, while in a utility network, a fault may affect customer reliability and regulatory performance.
Compare warranties carefully. A longer warranty has limited value if exclusions are broad, claims are slow, or the manufacturer has no practical ability to provide field support in the project region.
Procurement teams should use a weighted evaluation model that gives meaningful value to technical compliance, quality, schedule confidence, support capability, and lifecycle risk alongside commercial pricing.
This approach makes supplier selection easier to defend internally. It demonstrates that the chosen manufacturer offers the best overall project outcome rather than simply the lowest quoted equipment cost.
Confirm Commissioning, Spare Parts, and After-Sales Support
Support after shipment is a major differentiator between switchgear panel manufacturers. The real test of a supplier relationship often begins during installation, commissioning, troubleshooting, and the first years of operation.
Confirm whether the manufacturer provides site supervision, commissioning engineers, relay specialists, remote technical support, or training for operating and maintenance teams. Match the support package to project complexity.
For remote sites or international projects, ask about regional service partners, response times, language capability, travel arrangements, and availability of qualified personnel during critical energization windows.
Review the recommended spare-parts list and distinguish between commissioning spares, operational spares, and long-term strategic spares. The list should reflect actual component lead times and criticality.
Documentation quality directly affects maintainability. Require final single-line diagrams, schematics, terminal plans, wiring schedules, protection settings, test reports, operation manuals, and accurate as-built drawings.
Digital documentation should be searchable, version-controlled, and clearly linked to each panel identification number. Poor documentation extends fault-finding time and increases dependence on external technicians.
Ask how long the manufacturer can support installed products and whether obsolete components can be replaced with compatible upgrades. Long asset life is common in utility and industrial electrical systems.
Support commitments should be included in the contract, not left to informal assurances. Define scope, response expectations, warranty procedures, training requirements, and responsibilities for resolving defects discovered on site.
Use a Structured Supplier Evaluation and Decision Process
A structured process prevents decisions from being dominated by the most polished presentation or the lowest commercial offer. It also aligns engineering, procurement, operations, and project management stakeholders.
Begin with a mandatory compliance review. Eliminate suppliers that cannot meet essential electrical ratings, applicable standards, required certifications, delivery dates, or project-specific integration requirements.
Next, score qualified suppliers against weighted criteria. Typical categories include engineering competence, manufacturing quality, FAT capability, supply chain strength, references, lifecycle value, and after-sales support.
Use clarification meetings to test technical depth. Ask suppliers to explain their proposed design choices, known project risks, exceptions, manufacturing lead times, and support assumptions without relying only on prepared slides.
Reference checks should involve recent customers with similar operating conditions. Ask about design accuracy, delivery reliability, commissioning support, response to problems, and whether the supplier met commitments after payment.
Document technical deviations formally and evaluate their consequences. A minor variation may be acceptable, while an unrecognized deviation in fault rating, protection design, or enclosure classification can be unacceptable.
For high-risk projects, consider a pre-award factory audit, sample panel review, or pilot order. These steps add effort, but they can significantly reduce uncertainty before a large contract commitment.
The final recommendation should explain why the chosen switchgear panel manufacturer is suitable for the project’s technical, operational, commercial, and lifecycle requirements. This is stronger than simply listing comparative prices.
Final Decision: Choose Evidence Over Claims
The most reliable switchgear panel manufacturer is not necessarily the largest, cheapest, or most visible supplier. It is the one that can prove project fit through engineering evidence, controlled production, testing, delivery discipline, and support.
Project leaders should prioritize verified compliance, relevant references, transparent schedules, robust FAT procedures, documented quality controls, and practical post-commissioning support when comparing potential manufacturers.
A disciplined evaluation process reduces the likelihood of electrical faults, schedule overruns, redesign costs, site disputes, and operational interruptions. It also improves accountability across procurement and engineering teams.
When the decision is based on lifecycle value and demonstrated capability rather than quotation price alone, utility and industrial projects are better positioned for safe energization and dependable long-term performance.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.