Factory Modernization Cost vs Return: What to Evaluate Before Committing Budget
Why does factory modernization deserve a harder financial review now?
Factory modernization is rarely a simple equipment purchase. It usually changes productivity, maintenance patterns, energy use, staffing pressure, and operational resilience at the same time.
That is why capital approval cannot rely on a supplier quote alone. The real question is whether the upgrade creates durable return without locking operations into a long payback cycle.
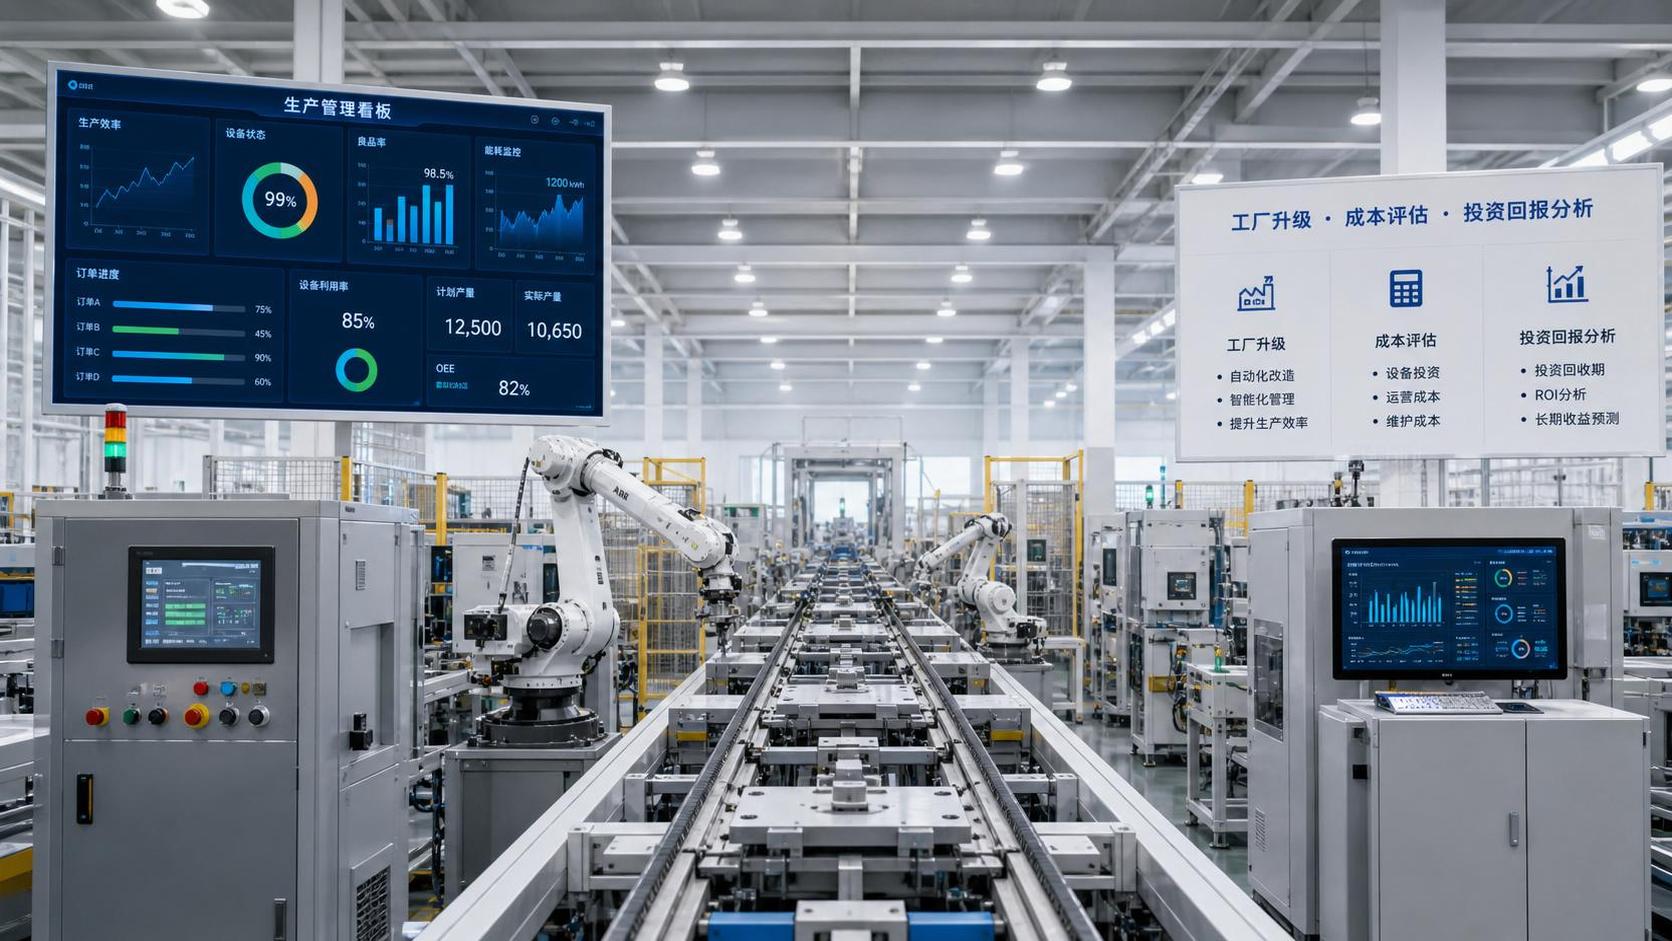
In practical terms, factory modernization may include machine replacement, automation layers, controls upgrades, electrical retrofits, digital monitoring, or line redesign.
Each option affects cost differently. Some reduce labor dependency. Others cut scrap, improve uptime, or lower power consumption. The financial case becomes credible only when those effects are measured line by line.
This is also where market intelligence matters. Industrial platforms such as NEXUSINSIGHTS help track equipment trends, supplier activity, trade signals, and technology adoption across manufacturing and automation sectors.
That broader context helps separate a needed modernization step from a fashionable one. A useful investment solves an operating constraint that already affects throughput, quality, cost, or risk.
What costs should be counted before approving factory modernization?
The quoted equipment price is only the visible part. A realistic factory modernization review needs the full landed and operating cost picture.
A common mistake is to compare one machine price against another. A better method is to map total investment from procurement through stable production.
- Core equipment, controls, drives, sensors, software, and integration licenses.
- Installation, civil work, electrical upgrades, utilities, safety systems, and commissioning.
- Production downtime during changeover, validation loss, and temporary output disruption.
- Training, process tuning, spare parts, service contracts, and cybersecurity support.
- Financing cost, import duties, compliance work, and possible redesign of upstream or downstream flow.
More hidden costs appear when modernization touches older lines. Legacy PLCs, incompatible interfaces, and unstable power quality can expand scope after approval.
For that reason, pre-investment audits are not administrative overhead. They are often the cheapest way to avoid budget drift.
The table below helps organize the most common questions before committing factory modernization budget.
How should return be measured beyond a simple payback estimate?
Payback period is useful, but it is too narrow on its own. Factory modernization often creates return through several smaller gains that compound over time.
A stronger review starts with baseline performance. Without a clean baseline, every expected gain becomes a debate after commissioning.
Look at measurable value in five areas.
- Output capacity: more units per hour, better utilization, or shorter changeover.
- Quality performance: reduced scrap, fewer rework hours, tighter process consistency.
- Operating cost: lower energy draw, reduced consumables, and less unplanned maintenance.
- Labor structure: fewer manual interventions and less dependence on hard-to-fill roles.
- Risk reduction: improved safety, compliance, traceability, and supply continuity.
Some returns are direct cash savings. Others protect margin by reducing interruptions that are expensive but irregular.
In actual factory modernization cases, uptime improvement can be more valuable than nominal speed increase. A faster line has little value if failures rise or support parts are hard to source.
It also helps to model three cases: conservative, expected, and aggressive. That makes board-level approval more disciplined and exposes whether the project still works under weaker assumptions.
When does factory modernization make more sense than patching existing assets?
This is often the hardest judgment. Older equipment may still run, but that does not mean it remains economical.
A repair-first approach usually works when failures are infrequent, spare parts are available, and the line still meets throughput, quality, and compliance targets.
Factory modernization becomes more compelling when one or more of these conditions appear.
- Maintenance spending is rising faster than output value.
- Manual workarounds are masking repeated bottlenecks.
- Energy intensity is materially above current market benchmarks.
- Obsolete controls create cybersecurity or support risks.
- Quality variation is affecting customer claims or downstream yield.
- Expansion plans depend on capacity the current line cannot deliver.
There is also a timing issue. Delaying modernization can feel prudent, yet delay may raise the eventual cost through rushed replacements, lost orders, or emergency procurement.
Sector tracking can sharpen this decision. NEXUSINSIGHTS, for example, is useful when checking how machinery pricing, automation adoption, and industrial supply chain shifts are moving across regions and categories.
What risks usually weaken the business case after approval?
Most failed modernization cases do not fail because the idea was wrong. They fail because assumptions were too optimistic or implementation discipline was too loose.
One frequent risk is overstated savings. If labor cannot actually be redeployed, headcount reduction should not be booked as immediate return.
Another issue is underestimating integration complexity. New automation may require MES changes, sensor recalibration, network segregation, or retraining that extends stabilization time.
Supplier concentration also deserves attention. A technically strong solution can still be risky when support depends on a narrow service footprint or proprietary components with long lead times.
Need to be careful with benchmark claims as well. Savings proven in one country, tariff structure, or shift pattern may not transfer directly to another site.
A practical risk screen should cover these points.
- Is the baseline data recent and audited?
- Are uptime and quality guarantees written into acceptance tests?
- Has the shutdown plan been tied to production commitments?
- Are spare parts and technical support available locally?
- Have energy, compliance, and cybersecurity implications been costed?
How can a capital review move from broad interest to a decision-ready case?
A solid factory modernization case is built in stages. It starts with the constraint, not the technology.
Define the problem in operating terms. Is the site losing output, margin, energy efficiency, or reliability? The answer determines what level of modernization is justified.
Then build a comparison across at least three options: maintain existing assets, retrofit selected systems, or complete modernization.
For each option, capture capex, downtime, expected savings, implementation time, technical dependence, and downside case. That comparison often reveals whether a partial upgrade delivers better value than a full replacement.
It is also useful to test assumptions against external market signals. Equipment availability, component lead times, policy changes, and supplier expansion activity can materially affect project timing and budget certainty.
In the end, factory modernization should be approved when the return logic is visible, the execution risk is bounded, and the upgrade clearly supports long-term operating performance.
The next practical step is to create a short evaluation sheet for baseline metrics, hidden costs, return drivers, and implementation risks. Once that is complete, supplier comparisons become much more reliable.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.