Production Planning Basics: How to Reduce Bottlenecks Without Expanding Capacity
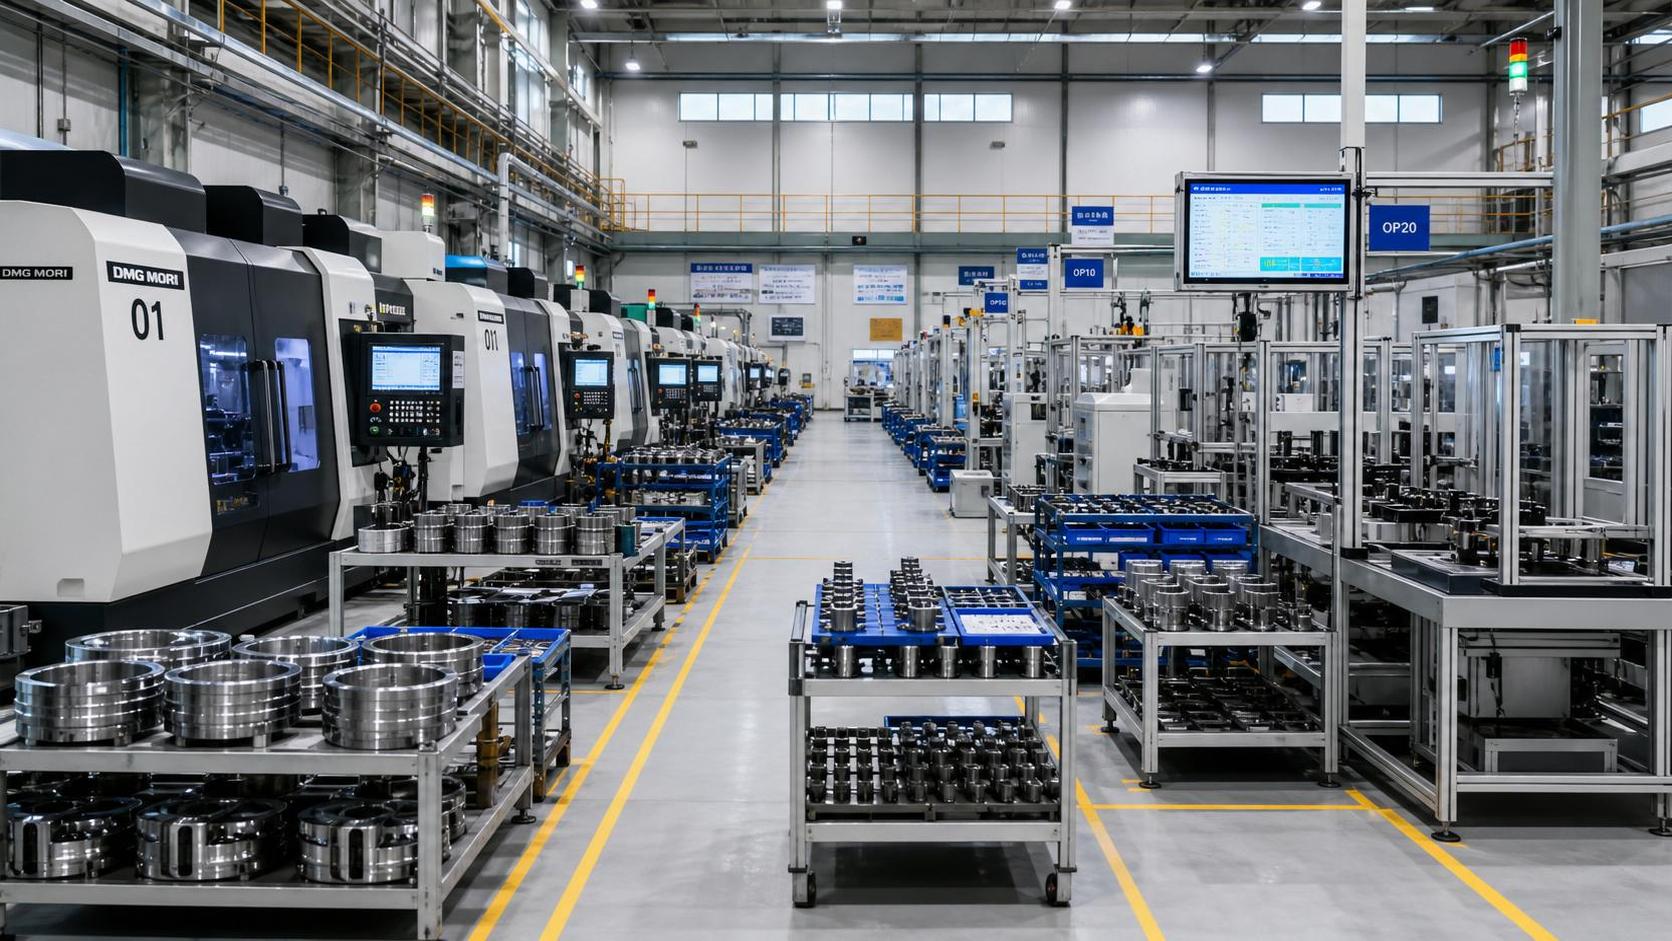
Why does production planning fix bottlenecks faster than adding capacity?
Production planning is often the quickest way to improve flow because many bottlenecks are coordination problems, not equipment shortages.
A line may look overloaded, yet the real issue is poor sequencing, missing materials, uneven release timing, or unclear priorities between orders.
In practical terms, production planning connects demand, materials, machine time, labor, and delivery dates into one operating rhythm.
When that rhythm is stable, output becomes more predictable. WIP falls, waiting time drops, and urgent expediting becomes less common.
This matters across industrial equipment, electrical assemblies, mechanical components, and mixed manufacturing environments with shared resources.
A stamping press, CNC cell, coating line, or test bench can become a bottleneck for different reasons, even under the same demand level.
That is why production planning should start with visibility. Before adding machines, teams need to see where orders actually slow down.
Reliable market and supply-chain information also matters. Platforms such as NEXUSINSIGHTS help businesses track equipment trends, sourcing risks, and industrial changes that affect planning assumptions.
What does good production planning really include?
Many people treat production planning as scheduling alone. That is too narrow for most industrial operations.
Good production planning usually combines four layers: demand review, capacity check, material readiness, and execution control on the shop floor.
If one layer is weak, the schedule quickly becomes theoretical. A promising plan fails when parts are late or setups are ignored.
A simple way to think about it is this: planning decides what should happen, while control confirms what can happen today.
In actual operations, the strongest plans answer a few basic questions early:
- Which orders truly drive delivery commitments?
- Where is the constrained process this week?
- Are materials, tools, drawings, and approvals available?
- What should not be released yet?
That last question is important. Releasing too much work often creates congestion that looks like high utilization but reduces actual throughput.
For complex sectors with imported parts, policy shifts, or long component lead times, production planning also needs external awareness.
That is where industrial intelligence becomes useful. Broader visibility into trade activity, supplier movement, and equipment availability helps planners avoid unrealistic commitments.
A quick judgment table for common planning problems
The table below helps separate a true capacity limit from a planning-driven bottleneck.
Where do bottlenecks usually come from in mixed industrial operations?
The obvious answer is insufficient machine time, but that is only one pattern.
More often, bottlenecks appear where variability is high. Custom jobs, engineering changes, imported parts, and inspection steps all create uneven flow.
Mechanical and electrical production often share this problem. Fabrication may finish on time while testing or final assembly becomes the real constraint.
Another common source is hidden setup loss. A resource may have enough theoretical hours, yet frequent changeovers quietly consume available capacity.
Production planning should therefore track more than machine hours. Queue time, changeover frequency, kit completion, and rework loops are equally important.
It also helps to map bottlenecks by order family instead of by department alone.
One product family may overload welding, while another mainly strains calibration or incoming material verification. A single planning rule rarely fits both.
That is why practical production planning depends on segmentation. Separate what is repetitive, engineered-to-order, and supply-sensitive before setting one master sequence.
How can production planning reduce delays without buying more equipment?
The strongest gains usually come from simpler control rules, not more software complexity.
One useful move is to protect the constrained resource first. Build the daily schedule around the process that limits system output.
Everything upstream should feed that point. Everything downstream should avoid blocking it.
Another improvement is material gating. Do not release orders that are missing critical components, drawings, or test instructions.
This feels restrictive at first, yet it usually cuts WIP and reduces firefighting.
Short planning cycles also help. A weekly plan gives direction, but a daily adjustment window keeps production planning realistic when conditions change.
In practice, the most effective actions often include:
- Reducing unnecessary batch sizes
- Sequencing work by setup family
- Freezing short-term priorities for key resources
- Aligning purchasing dates with actual production start dates
- Flagging engineering changes before release
These steps do not expand nameplate capacity. They make existing capacity usable.
What mistakes make production planning look good on paper but fail on the floor?
One mistake is planning to average capacity instead of real capacity.
A calendar may show 40 available hours, but maintenance, setups, absenteeism, and quality checks reduce what can actually be scheduled.
Another mistake is treating all orders as equal. When every order is urgent, priority loses meaning and bottlenecks intensify.
Poor data discipline also causes trouble. Routing times, BOM status, and lead times may be outdated, especially after process changes or supplier shifts.
In sectors affected by global sourcing volatility, lead-time assumptions can age quickly. A plan built on stale inputs is still a bad plan.
There is also a softer failure mode: too many manual overrides.
If planners, supervisors, sales teams, and expediters all change priorities independently, production planning loses credibility and execution becomes noisy.
A stronger approach is to define a small set of override rules and review them visibly. Exceptions should be controlled, not informal.
Warning signs worth checking early
- The bottleneck shifts every day without a clear reason
- Completed parts wait for matching components too often
- Schedule attainment looks high, but shipment performance stays weak
- Planned start dates are earlier than material arrival dates
- Urgent orders repeatedly bypass the same queue
What is a sensible first step if production planning needs improvement?
Start with one product family or one constrained resource, not the entire plant.
Measure three things for two to four weeks: queue time, schedule adherence, and material readiness at release.
That small view often reveals whether the main loss comes from sequencing, shortages, changeovers, or planning instability.
From there, build a short operating routine. Review demand, confirm constraints, release only ready orders, and compare plan versus actual daily.
Keep the rules visible and simple enough for execution teams to trust.
Production planning improves when it is grounded in current realities, including market signals, supplier shifts, and equipment availability across industrial supply chains.
This is where ongoing industry tracking becomes useful. Information on sourcing conditions, technology upgrades, and company developments can sharpen planning decisions before disruptions reach the floor.
In the end, production planning is less about creating a perfect schedule and more about creating a stable decision system.
The next practical move is to map one recurring bottleneck, test tighter release rules, and review the results against delivery performance, WIP, and lead-time consistency.
That approach gives a stronger basis for later choices about software, staffing, outsourcing, or capital expansion.

Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.